
Wood drying quality is an important factor in biomass processing, wood pellet production, briquette manufacturing, and other applications that use wood residues. Sawdust, wood chips, wood shavings, bark, and other wood materials often contain different levels of moisture. If this moisture is not properly controlled, it can affect grinding, pelletizing, fuel quality, storage stability, transportation, and overall production efficiency.
Good wood drying is not simply about reducing moisture. The material should be dried to a suitable and relatively uniform moisture level without excessive energy consumption or unnecessary damage to the biomass.
Many factors can affect drying quality. These include raw material type, initial moisture content, particle size, bulk density, drying temperature, airflow, residence time, feed rate, heat source, equipment design, moisture measurement, operator experience, and storage conditions.
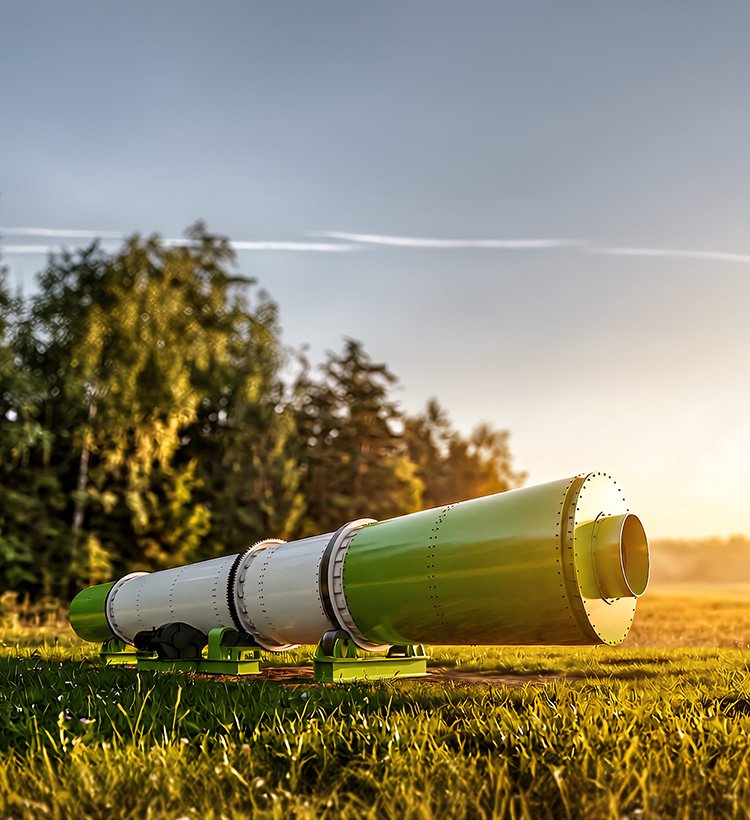
For commercial biomass plants, properly selected sawdust drying equipment can provide more stable moisture control and help prepare wood residues for downstream processing.
This article explains the major factors that affect wood drying quality and how each factor can influence the performance of a biomass drying system.
1. What Is Wood Drying Quality?
Wood drying quality refers to how effectively a drying process reduces moisture to the required level while maintaining relatively consistent material characteristics.
A high-quality drying process should achieve several objectives:
- Appropriate final moisture
- Uniform moisture distribution
- Stable production
- Reasonable energy consumption
- Low material loss
- Good downstream processability
- Suitable storage stability
The target depends on the application.
For example, sawdust used for wood pellet production needs to meet the moisture requirements of the pelletizing process. Wood used for direct combustion may have different requirements.
Therefore, there is no single moisture target suitable for every wood drying project.
2. Initial Moisture Content
Initial moisture is one of the most important factors affecting drying quality.
Sawdust produced from different sources may have very different moisture levels.
Freshly processed wood may contain significant moisture, while stored sawdust may be relatively dry.
The higher the initial moisture, the greater the amount of water that must be removed.
This affects:
- Drying time
- Heat consumption
- Dryer capacity
- Fuel consumption
- Airflow requirements
- Final moisture consistency
Before selecting drying equipment, the actual initial moisture should be tested.
Using an assumed moisture value can result in incorrect dryer sizing.
3. Final Moisture Requirement
The required final moisture is another important factor.
A biomass plant should determine why the material is being dried before selecting the drying parameters.
For example, the requirements may be different for:
- Wood pellets
- Biomass briquettes
- Boiler fuel
- Animal bedding
- Wood processing
- Long-term storage
The lower the target moisture, the more water must be removed.
However, excessively low moisture may not provide additional benefits and can increase energy consumption.
Therefore, efficient drying means achieving the required moisture rather than simply achieving the lowest possible moisture.
4. Moisture Uniformity
Final moisture content is not the only consideration.
Moisture uniformity is also important.
Imagine a batch of sawdust in which some particles are very dry while others remain wet.
The average moisture might appear acceptable, but the material may still cause problems during pelletizing.
Uneven moisture can result in:
- Variable pellet quality
- Unstable pellet mill operation
- Uneven storage performance
- Inconsistent fuel quality
A good drying system should therefore aim for both the correct average moisture and good moisture uniformity.
5. Wood Species
Different wood species have different physical structures and moisture characteristics.
Some types of wood release moisture more easily than others.
Density, fiber structure, resin content, and particle characteristics can all influence drying behavior.
When a biomass plant uses multiple wood species, operators may need to adjust drying parameters.
This is particularly important when raw material sources change frequently.
6. Particle Size
Particle size strongly affects drying quality.
Small sawdust particles have a relatively large surface area compared with their volume. This allows heat to contact more of the material surface.
Larger wood chips have a lower surface-area-to-volume ratio and may require longer drying conditions.
If particle sizes vary widely, drying may become uneven.
For this reason, crushing, grinding, and screening can improve the consistency of the feed material entering the dryer.
7. Excessively Fine Particles
Although smaller particles can dry efficiently, making the material extremely fine is not always beneficial.
Excessively fine sawdust may:
- Increase dust generation
- Increase material loss
- Increase dust collector load
- Raise safety requirements
- Increase fan power consumption
Therefore, particle size should be optimized according to the complete production process.
The best particle size is not necessarily the smallest one.
8. Bulk Density
Bulk density also affects drying.
Different biomass materials may occupy different volumes even when their weight is the same.
Sawdust, shavings, and wood chips have different bulk densities.
This affects how much material can move through a dryer and how air flows through the biomass.
If the material is too densely packed, hot air may not contact the particles evenly.
Proper material dispersion and dryer design are therefore important.
9. Drying Temperature
Temperature is one of the most important drying parameters.
Increasing temperature generally increases the potential rate of moisture evaporation.
However, excessive temperature can create problems.
It may:
- Waste energy
- Increase heat loss
- Affect biomass characteristics
- Increase fire risk
- Cause excessive material heating
Insufficient temperature may result in incomplete drying.
Therefore, the appropriate temperature should be determined according to the raw material and target moisture.
10. Airflow
Airflow plays two important roles.
First, it transfers heat to the biomass.
Second, it removes evaporated moisture.
If airflow is insufficient, humid air may remain around the material, reducing drying efficiency.
If airflow is excessive, energy consumption and dust carryover may increase.
The drying system should therefore balance:
- Fan capacity
- Air velocity
- Temperature
- Material flow
- Exhaust capacity
11. Airflow Distribution
The total airflow is important, but airflow distribution is equally important.
If some areas of the dryer receive more hot air than others, different parts of the material may dry at different rates.
This can result in uneven final moisture.
A properly designed dryer should distribute air as consistently as possible through the material.
This is one reason why dryer structure and internal design matter.
12. Residence Time
Residence time is the amount of time the material remains inside the dryer.
If residence time is too short, the material may leave before reaching the target moisture.
If it is too long, the material may be over-dried.
Residence time is affected by:
- Dryer dimensions
- Drum speed
- Material feed rate
- Airflow
- Particle size
- Material density
- Initial moisture
A stable residence time contributes to more consistent drying.
13. Feed Rate
Feed rate determines how much biomass enters the drying system per unit of time.
If the feed rate is too high, the dryer may not have enough heat-transfer capacity to remove the required moisture.
This can cause wet material to leave the dryer.
If the feed rate is too low, the equipment may not operate efficiently.
Automatic or controlled feeding can improve drying stability.
14. Heat Source Stability
A stable heat source is essential for good drying quality.
The heat source may use:
- Biomass fuel
- Natural gas
- Diesel
- Other suitable fuels
- Waste heat
If the heat supply fluctuates significantly, the drying temperature can also change.
This can produce variable final moisture.
Therefore, the heating system should provide sufficient and stable thermal energy.
15. Heat Source Efficiency
The efficiency of the heat source affects the overall drying process.
An inefficient combustion system may consume more fuel while providing less useful heat.
A properly designed heat source should provide:
- Stable temperature
- Adequate thermal capacity
- Controlled combustion
- Appropriate heat transfer
- Safe operation
For biomass drying projects, using suitable biomass residues as fuel can sometimes improve energy economics.
16. Dryer Design
The design of the dryer has a major influence on drying quality.
Important design characteristics include:
- Dryer dimensions
- Internal structure
- Material lifting system
- Airflow direction
- Feeding system
- Discharge system
- Heat distribution
- Exhaust design
For continuous industrial drying, the dryer must be designed around the actual material and capacity.
A dryer designed for one type of biomass may not perform equally well with another.
17. Choosing the Right Sawdust Drying Equipment
Selecting suitable sawdust drying equipment is essential for consistent drying.
The equipment should be evaluated based on:
- Raw material
- Initial moisture
- Target moisture
- Particle size
- Capacity
- Heat source
- Factory layout
- Energy availability
- Automation requirements
- Dust collection requirements
A buyer should avoid selecting equipment based only on a nominal tons-per-hour figure.
The actual moisture evaporation capacity is more important.
(Learn more:https://pelletisingmachine.com/sawdust-dryer-machine/)
18. Dryer Capacity
Dryer capacity should be calculated according to the actual water removal requirement.
For example, two plants may both process the same amount of wet sawdust per hour but require very different drying capacities if their initial moisture contents are different.
A proper calculation should consider:
- Wet feed rate
- Initial moisture
- Target moisture
- Water evaporation
- Operating hours
This helps prevent undersized or oversized equipment.
19. Material Feeding System
A good dryer requires a stable feeding system.
Possible feeding equipment includes:
- Screw conveyor
- Belt conveyor
- Rotary feeder
- Hopper
- Metering feeder
The feeding system should minimize fluctuations.
Sudden changes in feed rate can lead to changes in final moisture.
Stable feeding also helps the heat source operate under more consistent conditions.
20. Moisture Measurement
Accurate moisture measurement is essential for controlling drying quality.
Moisture should be checked at different stages.
Important points include:
- Raw material inlet
- Dryer outlet
- Finished product
- Storage or pelletizing feed
Online moisture sensors can provide continuous monitoring.
Laboratory testing can also be used for verification.
Using both methods can improve process control.
21. Operator Experience
Operators play an important role in drying quality.
They need to understand how changes in raw material affect drying.
For example, if the incoming sawdust suddenly becomes wetter, the operator may need to adjust:
- Feed rate
- Temperature
- Airflow
- Residence time
An experienced operator can identify unusual conditions quickly.
However, automation can reduce dependence on manual adjustment.
22. Automation and Control
Modern drying systems can use centralized control systems.
The system can monitor:
- Temperature
- Feed rate
- Fan status
- Exhaust temperature
- Material flow
- Moisture
- Heat source
Automatic control can adjust operating parameters according to process conditions.
This improves repeatability and reduces operator workload.
23. Exhaust System
The exhaust system removes moisture-laden air from the dryer.
A properly designed exhaust system helps maintain airflow and drying efficiency.
It may include:
- Exhaust fan
- Ducting
- Cyclone
- Dust collector
- Air filtration equipment
If the exhaust system is undersized, humid air may not be removed effectively.
If it is oversized, excessive heat and fine particles may be lost.
24. Dust Collection
Sawdust drying can generate fine particles.
A suitable dust collection system helps control these particles.
It can also reduce the amount of biomass lost through the exhaust system.
Important components may include:
- Cyclone separator
- Bag filter
- Dust collector
- Exhaust fan
Dust collection should be designed according to the material and airflow conditions.
25. Heat Loss
Heat loss reduces drying efficiency.
Common sources include:
- Poor equipment insulation
- Unnecessary openings
- Long hot-air ducts
- Poorly sealed connections
- Inefficient exhaust
Good insulation can help maintain the required temperature while reducing fuel consumption.
This is especially important for continuous industrial operation.
26. Dryer Maintenance
Equipment condition directly affects drying quality.
Worn or damaged components can reduce performance.
Important inspection areas include:
- Bearings
- Drum
- Drive system
- Fans
- Feeders
- Conveyors
- Furnace
- Sensors
- Dust collectors
- Ducts
Regular preventive maintenance can help keep the dryer operating consistently.
27. Storage Before Drying
Raw material storage can affect drying quality.
If wet sawdust is stored under unsuitable conditions, its moisture may change.
It may also experience:
- Heating
- Biological activity
- Mold growth
- Odor
- Material degradation
Proper storage before drying helps maintain more predictable raw material conditions.
28. Storage After Drying
Dried biomass can absorb moisture again if exposed to humid conditions.
This is especially important in regions with high humidity.
Dried material should therefore be transferred efficiently to:
- Pelletizing
- Briquetting
- Fuel production
- Protected storage
Storage facilities should be dry, clean, and appropriately ventilated.
29. Weather and Seasonal Conditions
Environmental conditions can affect wood drying.
For example, ambient humidity can influence the moisture content of raw material and the ability of the drying system to remove water.
Seasonal changes may also affect:
- Raw material moisture
- Heat requirements
- Storage conditions
- Cooling performance
A commercial plant should be designed to handle expected seasonal variations.
30. Initial Material Temperature
The temperature of the incoming biomass can also influence drying.
Material entering the dryer at a low temperature requires some heat simply to increase its temperature before significant moisture evaporation occurs.
This means environmental conditions and raw material storage can affect thermal requirements.
31. Moisture Reabsorption During Conveying
Even after drying, biomass may absorb moisture during conveying.
Long conveying distances and open-air transfer can increase exposure to humid air.
Therefore, the transfer system between dryer and pellet mill should be designed to minimize unnecessary exposure.
Covered conveyors and enclosed transfer systems can be useful in humid environments.
32. Drying Quality and Pellet Production
For wood pellet plants, drying quality has a direct relationship with pellet production.
If sawdust moisture is too high, the pellet mill may experience:
- Reduced output
- Higher energy consumption
- Poor pellet formation
- Increased fines
If the material is too dry, pellet formation may also become less stable.
Therefore, the drying process should prepare the sawdust for the specific pelletizing conditions.
33. Drying Quality and Pellet Durability
Pellet durability is affected by many factors, including moisture.
Appropriate moisture can help the material form stronger pellets under compression.
However, durability also depends on:
- Particle size
- Wood species
- Pellet mill design
- Die compression ratio
- Roller condition
- Feed rate
- Conditioning
- Cooling
Drying should therefore be optimized together with pelletizing.
34. Drying Quality and Fuel Value
For biomass fuel, excessive moisture reduces the useful energy available during combustion.
More energy must be used to evaporate water before the fuel can release its full combustion energy.
Proper drying can therefore improve the practical fuel quality of wood residues.
For pellet manufacturers, controlled moisture also helps produce a more consistent finished product.
35. Common Drying Quality Problems
Uneven Moisture
Possible causes include:
- Uneven particle size
- Poor airflow distribution
- Unstable feeding
- Inconsistent raw material
Excessive Moisture
Possible causes include:
- Insufficient heat
- Excessive feed rate
- Short residence time
- High initial moisture
Over-Drying
Possible causes include:
- Excessive heat
- Low feed rate
- Long residence time
- Incorrect control settings
High Dust Loss
Possible causes include:
- Excessive airflow
- Very fine particles
- Poor dust collection
- Improper exhaust settings
Each problem should be diagnosed based on actual process data.
36. How to Improve Wood Drying Quality
Several measures can improve drying quality:
- Test incoming moisture regularly.
- Control particle size.
- Maintain stable feeding.
- Set an appropriate moisture target.
- Control temperature.
- Maintain suitable airflow.
- Optimize residence time.
- Use a stable heat source.
- Monitor outlet moisture.
- Maintain the dryer regularly.
- Improve insulation.
- Control dust.
- Prevent moisture reabsorption.
- Use automatic process control.
These measures work together to create a more stable drying process.
37. How to Choose a Drying System for a Wood Pellet Plant
When planning a wood pellet plant, the drying system should be designed around the complete process.
A typical process may be:
Raw Material Receiving → Chipping → Grinding → Drying → Pelletizing → Cooling → Screening → Packing
The drying system should be matched to the pellet mill capacity.
For example, if the pellet mill requires a stable supply of dried sawdust, the dryer must provide sufficient output even when raw material moisture reaches its expected maximum.
This prevents the dryer from becoming a bottleneck.
38. Why Complete Process Design Matters
Drying quality cannot be evaluated independently from other processing stages.
Grinding affects particle size.
Particle size affects drying.
Drying affects pelletizing.
Pelletizing affects cooling.
Cooling affects storage.
Therefore, all stages should be considered together.
A complete engineering approach can help optimize the relationship between:
- Raw materials
- Grinding
- Drying
- Pelletizing
- Cooling
- Screening
- Packing
39. RICHI Sawdust Drying Solutions
RICHI Machinery provides biomass processing equipment and turnkey engineering solutions for wood and biomass processing projects.
For a sawdust drying project, RICHI can evaluate:
- Raw material type
- Initial moisture
- Target moisture
- Particle size
- Required capacity
- Heat source
- Factory layout
- Pellet specifications
- Automation requirements
A complete system can include:
- Wood chipper
- Hammer mill
- Sawdust drying equipment
- Pellet mill
- Pellet cooler
- Screening machine
- Packing machine
- Conveyors
- Dust collection system
- Electrical control system
The equipment configuration can be customized according to the customer’s actual production requirements.
40. A Practical Checklist for Better Wood Drying Quality
Before building or upgrading a drying system, consider the following questions:
Raw Material
- What type of wood residue is available?
- What is the average moisture?
- What is the maximum moisture?
- Is the particle size consistent?
Production
- What is the required capacity?
- What final moisture is required?
- How many hours will the plant operate each day?
Equipment
- What type of dryer is suitable?
- What heat source is available?
- What dust collection system is required?
- Is automatic control needed?
Downstream Process
- Will the dried material enter a pellet mill?
- What pellet diameter is required?
- Is buffer storage necessary?
- How will the material be cooled and stored?
Answering these questions before equipment selection can significantly improve the final drying system.
Frequently Asked Questions
What factors affect wood drying quality?
The major factors include initial moisture, target moisture, wood species, particle size, bulk density, drying temperature, airflow, residence time, feed rate, heat source, dryer design, moisture measurement, maintenance, and storage conditions.
What is sawdust drying equipment used for?
Sawdust drying equipment is used to reduce the moisture content of sawdust and other biomass materials before pelletizing, briquetting, fuel production, or storage.
Does particle size affect sawdust drying?
Yes. Particle size affects heat transfer and moisture evaporation. More uniform particles generally make drying more predictable.
Does higher drying temperature always improve drying quality?
No. Excessive temperature can waste energy and create safety or material-quality problems. Temperature should be controlled according to the raw material and target moisture.
Why is moisture uniformity important?
Uniform moisture helps create stable downstream processing conditions. In wood pellet production, it can contribute to more consistent pellet formation and production performance.
How do I choose suitable sawdust drying equipment?
Consider initial moisture, target moisture, particle size, capacity, heat source, energy consumption, dust collection, automation, and downstream equipment.
Can wet sawdust be stored before drying?
It can be stored, but storage conditions should be carefully managed. Excessive moisture and unsuitable storage can cause heating, biological activity, or material deterioration.
How does drying affect wood pellet production?
Proper drying can improve pellet mill stability, pellet formation, pellet durability, and production consistency when the raw material has excessive or unstable moisture.
Is automatic moisture control necessary?
It is not always necessary for small operations, but automatic moisture monitoring and control can be very useful for commercial plants with variable raw material moisture.
Conclusion
Wood drying quality is influenced by many interconnected factors. Initial moisture, final moisture requirements, wood species, particle size, bulk density, temperature, airflow, residence time, feed rate, heat source, dryer design, moisture measurement, and equipment maintenance all affect the final result.
For biomass pellet production, moisture control is particularly important because the dried sawdust must provide stable conditions for pelletizing. Excessively wet or excessively dry material can reduce production efficiency and affect pellet quality.
Properly selected sawdust drying equipment can provide stable moisture control, but equipment selection should always be based on the complete project requirements. Initial moisture, target moisture, evaporation capacity, particle size, heat source, production capacity, dust collection, and downstream pellet mill capacity should all be considered.
The most effective approach is to treat wood drying as part of an integrated biomass processing system. By combining accurate moisture measurement, stable feeding, optimized temperature and airflow, proper residence time, efficient heat management, regular maintenance, and suitable automation, biomass manufacturers can achieve more consistent drying quality while improving overall production efficiency.